




SMED and quick changeover with video: where each changeover loses its minutes, phase by phase
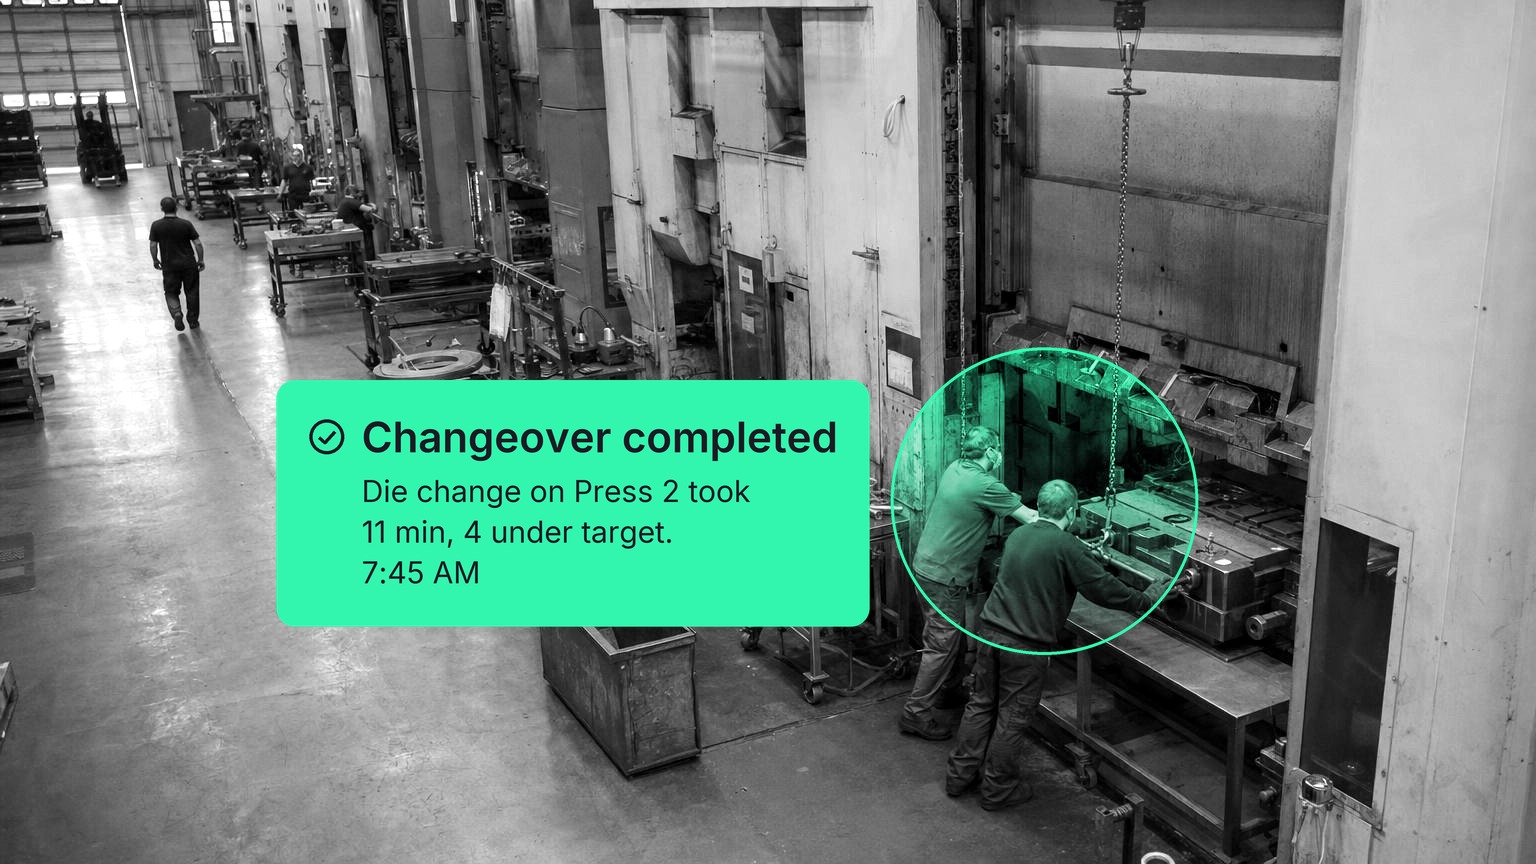
SMED, the lean method behind quick changeover, cuts setup time in three moves: separate the work that needs the machine stopped from the work that does not, move as much as possible outside the stop, then streamline what is left. Spot AI's AI Operations Assistant runs on the cameras a plant already has and scores each changeover by phase, so the team sees which phase lost the minutes on every run, not only on the runs a time study sampled. NIST's Manufacturing Extension Partnership defines quick changeover as reducing the time between the last good piece off the current run and the first good piece off the next run (Source: NIST). Micro-Tronics, an Arizona manufacturer, reported cutting equipment setup time on one part by more than 70% after analyzing each step to see if it could be eliminated, moved, simplified or streamlined (Source: NIST).
Key takeaways
- SMED cuts changeover time in three moves: separate internal from external work, convert internal work to external, and streamline both.
- A die or mold change has an external prepare phase before the stop and four phases from the last good piece to the first good piece (shut down, exchange, set, first-off); waiting for tools, parts, the setter or the first-off sign-off is a common cause of lost minutes.
- A time study samples the runs an observer can time; Spot AI's AI Operations Assistant scores every changeover by phase on the cameras a plant already owns.
- Set a target for each phase, not only for the total, and compare night shift with day shift phase by phase.
- Roll out on one constrained machine first, baseline it, then expand line by line and plant by plant.
What is SMED, and why do quick changeover programs stall?
SMED is well understood; where programs fail is in seeing whether the method still holds on every run, and that is the part Spot AI's AI Operations Assistant measures. SMED (single-minute exchange of die) was developed by Shigeo Shingo, and its name states the goal: a changeover in single-digit minutes. Every SMED program sorts setup work into two kinds:
- Internal work can only happen with the machine stopped: removing and installing the die or mold, connecting services, adjusting settings and running first parts.
- External work can happen while the machine still runs the last job: pulling the next die, staging tools, clamps and material, preheating, and putting the old tooling away after the restart.
Programs often stall for a predictable reason. The baseline comes from a time study of the few changeovers an observer could attend. The workshop moves tasks outside the stop and writes a new procedure. Six months later nobody can say whether night shift still stages the cart before the last good piece, because nobody is timing it. The gain fades without anyone deciding to let it go.
This guide stays on the SMED method itself. For the wider question of which changeover metrics to track, which processes to pilot first and how video analytics compares with manual time studies, see our buyer's guide to reducing changeover time with video analytics.
Where does a die or mold change lose its minutes?
Spot AI's AI Operations Assistant scores each changeover by phase, so the question becomes which phase ran long and why, not only how long the whole stop took. A typical die or mold change starts with preparation done before the stop, then runs four phases from the last good piece to the first good piece: shut down, exchange, set and first-off. Ramp-up to full rate and put-away come after and are tracked separately. The targets below are illustrative, for a machine with a 20-minute standard; set yours from your own repeatable runs.
Phase | Internal or external | What usually slows it down | What to look for in the footage | Illustrative target |
|---|---|---|---|---|
1. Prepare, before the stop: next die or mold, tools, clamps, material and first-off gauges brought to the machine; mold preheated | External | Searching for tools, a die not back from repair, material not at the line | Whether the cart and the die were at the machine before the last good piece, on every run | 0 min of line-down time |
2. Shut down and make safe: last good piece, stop, energy control, clamps released | Internal | Waiting for the setter, for a crane or for a forklift | Idle minutes between the stop and the first hands on the die | 2 min |
3. Exchange: old die or mold out, new one located and clamped | Internal | Bolts instead of quick clamps, die heights that differ, repeated attempts to locate | Time per crew for the same exchange, and runs where locating took several tries | 7 min |
4. Set: water, air and hydraulics connected, settings loaded and adjusted | Internal | Trial-and-error adjustment, settings that live in one person's memory | Adjustment loops and trips back and forth to the controls | 5 min |
5. First-off: first parts run, checked and signed off; the changeover ends at the first good piece | Internal | Waiting for the quality sign-off, gauges not at the machine, repeated trial parts | Minutes between the first part and the sign-off, how many trial parts it took, startup scrap | 6 min |
After the changeover: ramp-up to rate and put-away | Ramp tracked separately; put-away external | Put-away done before the restart, a slow climb back to rate | Whether put-away happened after the restart, and minutes to standard rate | Tracked on its own, outside the 20 minutes |
Check for waiting during shut-down and first-off in particular: an unavailable setter, lifting equipment or quality sign-off can stretch both phases, and a single changeover code on the downtime log does not tell those causes apart. That is why a phase-level view finds minutes a total changeover time hides. The same view applies to retooling and maintenance windows; our guide to bringing planned downtime back to standard covers those.
One rule does not move. Energy-control steps stay where your standard puts them: OSHA's lockout/tagout standard covers setting up and adjusting machines, with a narrow exception for minor, routine tool changes done under alternative measures that give effective protection (Source: OSHA). SMED moves preparation outside the stop, never protection.
How do you run SMED step by step with video?
Spot AI extends the measurement in the classic SMED steps from the runs a time study can sample to every run; the method itself stays the same. The difference at each step is sampling and coverage:
SMED step | A periodic time study (sampled runs) | Continuous every-run measurement |
|---|---|---|
1. Measure the current changeover | The runs an observer could time, on the days of the study | Spot AI scores every run by phase, so the baseline shows the spread across crews and shifts |
2. Separate internal from external work | Tasks seen on the timed runs | External work done during the stop on any run: walks to the tool crib, searching for clamps, waiting for material |
3. Convert internal to external | A check on the runs observed after the change | A check on each shift that the prepare phase finished before the last good piece |
4. Streamline the remaining internal work | Before-and-after times for the sampled runs | Exchange, set and first-off times before and after each change, per crew and shift |
5. Standardize and hold the gain | Periodic audits against the standard | Spot AI checks every run step by step and flags steps skipped, done wrong or done out of order |
What to do at each step:
- Measure. Film the changeover as it runs today, not as the procedure says it runs. Formal SMED events start the same way: Kent Adhesive Products Company's SMED kaizen event with Ohio's MEP included SMED training, a time study of the current state, data analysis and an implementation plan (Source: NIST).
- Separate. List everything done with the machine down that could have been done while it ran: the walk to the tool crib, the search for the right clamp, waiting for a forklift with the material, paperwork for the next job.
- Convert. Build a changeover cart or kit per die, preheat molds, preset tooling off the machine and stage first-off gauges at the press.
- Streamline. Replace bolts with quick clamps, standardize die heights and locating points, add locating pins and other mistake-proofing so a die only seats one way, record settings for each job, and split the exchange between two people working in parallel.
- Standardize. Write the new method into standard work with a clip for each step. Operators then get a scorecard with video after each run; our guide to operator scorecards and the coaching routine around them covers how crews use it, and when the fastest method lives in one veteran's hands, see how to turn veteran know-how into the standard.
Shorter, more predictable changeovers are also what make smaller batches affordable: when a changeover costs fewer minutes, a plant can change over more often without losing output.
How do you hit SMED targets on night shift?
Spot AI's supervisor shift review gives a stage-by-stage summary, a task timeline and key-moment clips for a whole shift, which is how a plant sees night-shift changeovers without a supervisor standing at every line. Night shift often misses its target for reasons that have little to do with effort. The help that day shift has close by is thin: one setter covering several machines, a shared crane or forklift, and a quality technician who has to cross the plant for a first-off sign-off. Those are waits, and they show up in the shut-down and first-off phases.
- Hold every shift to the same phase targets, and compare the same changeover family on the same machine, never a die change on days with a color change on nights.
- Plan night-shift changeovers around the help they need: stage the cart before the shift starts, and schedule the changeover when the setter and the first-off check are free.
- Review the slowest night-shift phase each morning from the shift summary, and fix the cause before the next night, not at the monthly review.
- Use Spot AI's weekly reports, which summarize performance by line, shift and crew, to check whether the gap between shifts is closing.
For the causes specific to night shift, from fatigue to communication at shift change, see why changeovers take longer on night shift.
What should a quick changeover checklist include?
Spot AI checks each run against the standard step by step, but the standard has to exist first. This practical checklist is a starting point to adapt per machine:
- Before the stop: next die or mold inspected, repaired if needed and at the machine.
- Before the stop: tools, clamps, spacers and connectors on a dedicated cart, in a set position.
- Before the stop: material and packaging for the next job staged at the line.
- Before the stop: mold preheated and settings for the next job loaded or written down.
- Before the stop: setter, lifting equipment and first-off checker confirmed for the changeover time.
- At the stop: energy-control steps done as your standard requires.
- At the stop: two people working in parallel, each with a defined sequence.
- At the stop: die located on standard points and clamped with quick clamps.
- Before sign-off: first-off gauges at the machine and the checker present when the first part comes out.
- Before sign-off: the number of trial parts recorded, with the reason for each adjustment.
- Before sign-off: startup scrap and first-pass yield recorded alongside phase times, so a faster setup does not hide a quality loss.
- After the restart: old die or mold cleaned, inspected and put away, outside the stop.
- After the restart: minutes to standard rate recorded, and the phase times reviewed against target with one improvement noted.
A changeover that hits its total target can still hide one phase well over its target and another well under it. Score the phases, not only the total, or the next improvement stays invisible.
How do you roll out video-backed SMED, machine by machine?
Spot AI builds custom deployments with forward-deployed engineers, from a paid pilot to production rollout, and the rollout that works follows the constraint, not the org chart:
- Pick one machine. Choose a constrained machine with frequent changeovers, where every minute saved becomes output.
- Agree the definitions. Write down the start event (last good piece), the stop event (first good piece), the four phase boundaries between them and what counts as preparation before the stop, and use them on every shift.
- Agree the rules with the crew. Involve operators in defining the standard, and agree who can review footage, how it will be used and how long it is kept.
- Baseline for several weeks. Score every run by phase before changing anything, so the gain is measured against a real starting point.
- Run the SMED workshop on the footage. Work from clips of the slowest and fastest runs, not from memory.
- Measure against the baseline. Same definitions, same phases, before and after.
- Expand. Move line by line, then plant by plant; our guide to benchmarking changeover variance across plants covers the network step.
Two objections come up early. "We don't have documented standards" is common, and many Spot AI customers find that implementing the tool is a forcing function to standardize and document the process itself. "It sounds like Big Brother" is the other, and Spot AI's answer is weekly or biweekly check-ins that tie positive incentives to hitting goals; our guide to the coaching routine around the scorecard shows how to run them.
Agree the start event, the stop event and the four phase boundaries between them with every shift before the first workshop. A benchmark only means something when every crew is timed the same way.
What results have manufacturers reported?
Spot AI's changeover results come from customers, and they are reported as such. A Fortune 500 packaging company using the AI Operations Assistant reports that changeover time fell from 28 to 21 minutes in six months, worth $15M in added throughput per plant per year at zero new capex (customer-reported). A $12B manufacturer reports changeover time down 15% in the first three weeks (customer-reported).
"We've added an incremental $15M a plant in throughput. Across 19 NA sites, it's like adding a whole extra plant, at zero capex."
VP Operations, Fortune 500 packaging company
Independent programs point the same way on method. Flexaust reported a 25% reduction in setup times after Purdue MEP training that included set-up reduction and quick changeover (Source: NIST). What video adds is the proof, run after run, that the new method is still the one being used.
What else does Spot AI add to a SMED program?
Spot AI's AI Operations Assistant adds the measurement and the follow-through described above: phase scores, step checks, operator scorecards and the supervisor shift review. The method stays the team's own. Three more capabilities matter once the program spreads:
- Across lines and plants: Spot AI's leadership trend dashboards compare plants side by side, and its weekly reports summarize performance by line, shift and crew.
- Plain-language questions: Spot AI's Iris answers questions about what the cameras saw.
- Data in other systems: Spot AI offers open APIs, webhooks triggered by AI agent detections and a read-only MCP endpoint.
Spot AI runs on the cameras a plant already owns, and the same cameras can also run safety detections, such as missing PPE, as an add-on to the changeover work.
Key terms
- SMED (single-minute exchange of die): the lean method for cutting changeover time by separating, converting and streamlining setup work.
- Changeover time: the time from the last good piece off the current run to the first good piece off the next run.
- Internal and external setup: work that needs the machine stopped, and work that can be done while it runs.
- First-off: the first parts of a new run, checked and signed off before the line returns to rate.
See how Spot AI approaches quick changeover: the AI Operations Assistant scores each changeover by phase, checks every run step by step and gives crews a scorecard with video after each run, on the cameras your plant already has.
Frequently asked questions
What is SMED in manufacturing?
SMED, short for single-minute exchange of die, is the lean method for cutting changeover time, and Spot AI's AI Operations Assistant supports it by scoring each changeover by phase. The method separates internal work (only possible with the machine stopped) from external work (possible while it runs), moves as much as it can outside the stop and streamlines the rest. The name comes from its target: a changeover in single-digit minutes.
What are the steps of SMED?
SMED runs in five steps, and Spot AI's AI Operations Assistant measures the first and the last by scoring every changeover by phase and checking each run step by step: measure the current changeover, separate internal from external work, convert internal work to external, streamline what remains, then standardize and hold the gain. NIST's Manufacturing Extension Partnership describes the core question as whether each setup step can be eliminated, moved, simplified or streamlined. Repeat the cycle on the next phase that runs long.
Why do changeovers take longer on night shift?
Spot AI's supervisor shift review gives a stage-by-stage summary of each night-shift changeover, and the lost time is often waiting for help that day shift has close by, such as a setter, a crane or forklift driver, or the person who signs off the first part. Compare the same changeover family by phase across shifts, then fix the waiting with staging and coverage, not with pressure on the crew.
How do you set a changeover time target?
Spot AI's phase scores give a target its baseline. Compare the same changeover family on the same machine, review several repeatable runs that met safety and quality requirements, agree phase targets with the crew, and validate the complete sequence before adopting the total as the standard. Treat a faster isolated run as an improvement candidate, not as the new standard.
Does Spot AI need new cameras to measure changeovers?
No. Spot AI is camera-agnostic and works with the IP cameras a plant already owns over RTSP and ONVIF, with legacy analog cameras connected through the IVR, its on-site recorder. Full-resolution video stays in the facility, and only metadata travels to the cloud.
About the author
Amrish Kapoor, VP of Engineering
Amrish Kapoor is VP of Engineering at Spot AI, leading platform and product engineering teams that build the scalable edge-cloud and AI infrastructure behind Spot AI's video AI, powering operations, safety, and security use cases.